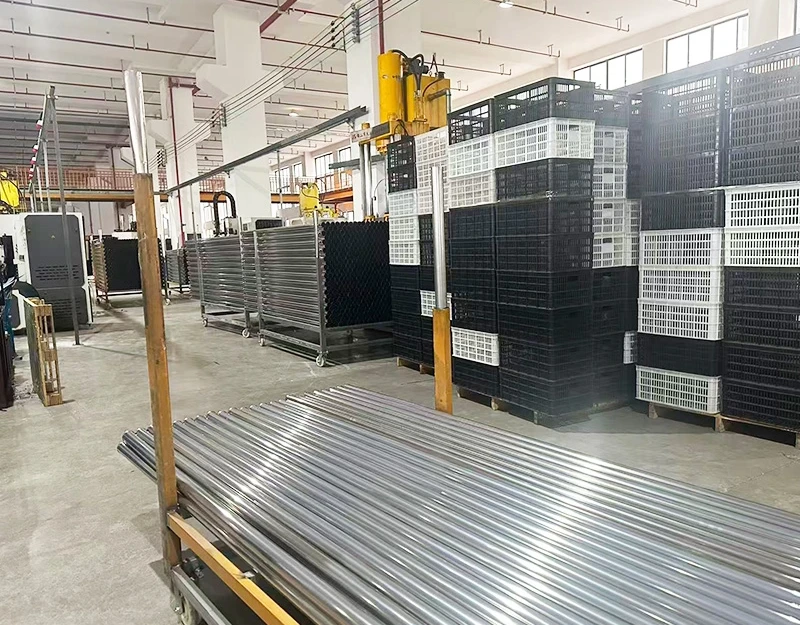
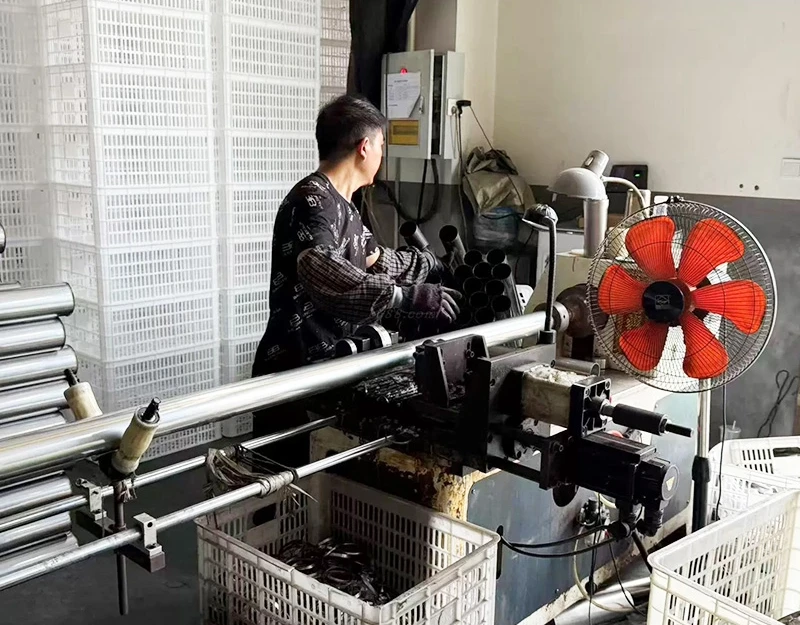
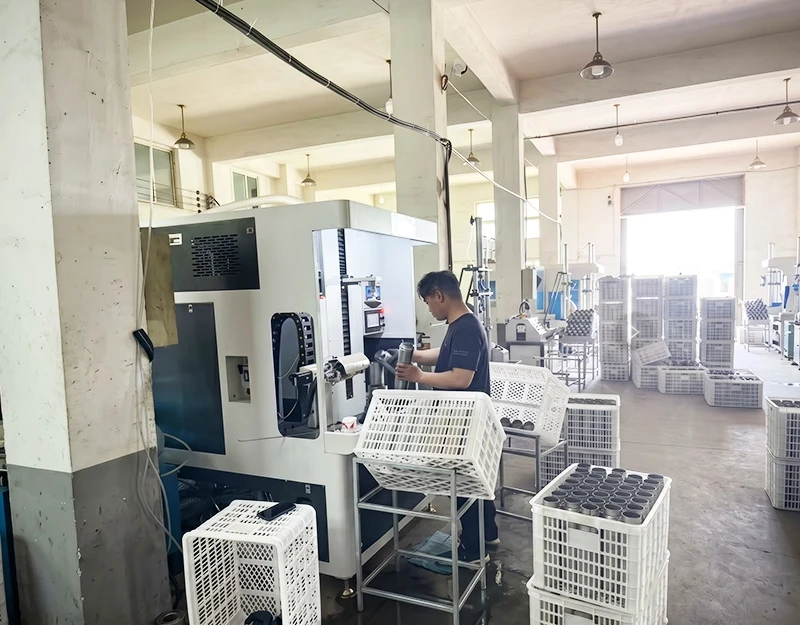
Our team controls the production process in-house, from material selection to final inspection. That means stable quality, reliable lead times and a clear point of contact for every wholesale drinkware order.
01
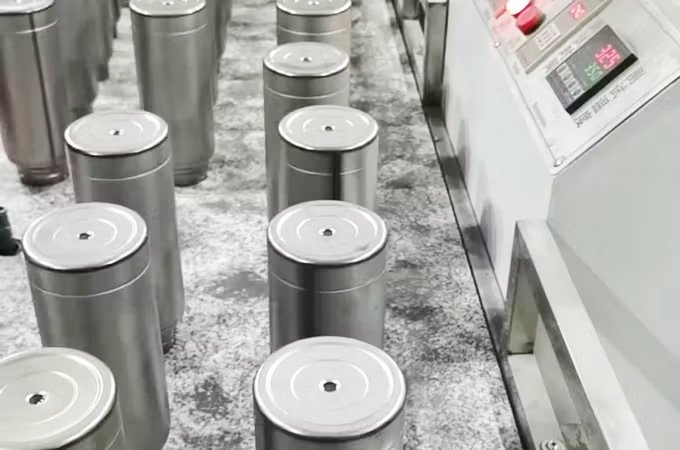
Raw material preparation
Qualified materials, ready to perform.
Food-grade stainless steel and approved components are checked before production begins.
02
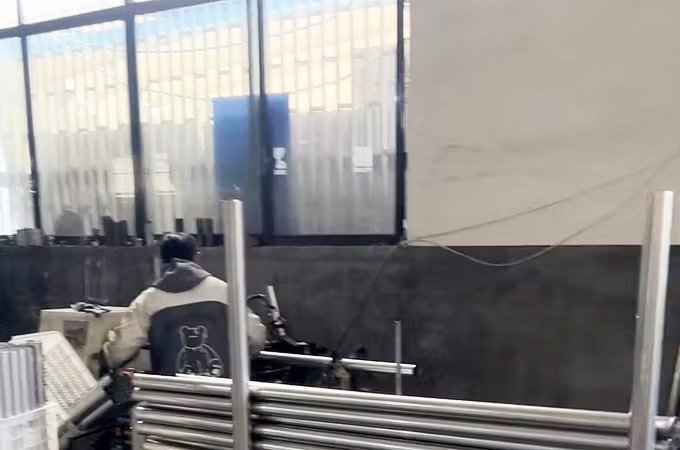
Tube cutting & forming
Precise dimensions from the start.
Sheets are cut, shaped and formed into inner and outer shells with repeatable tolerances.
03
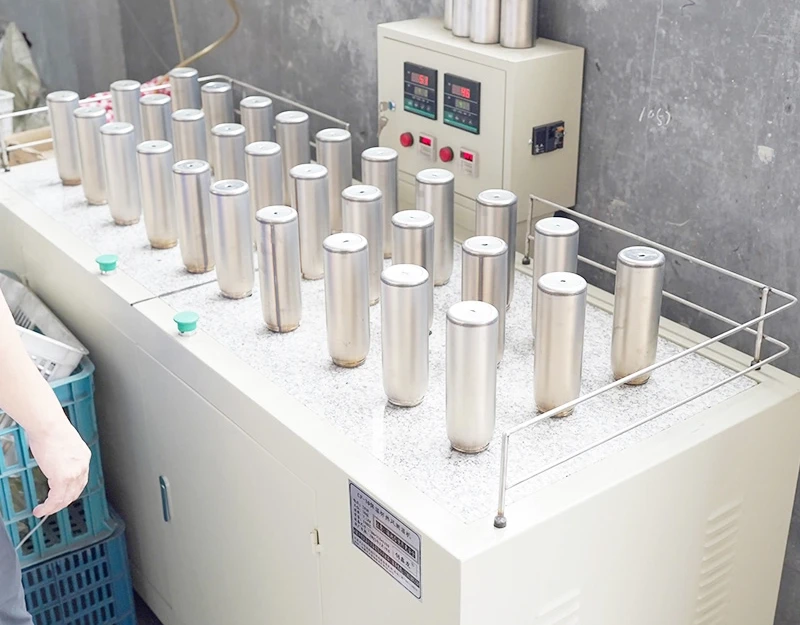
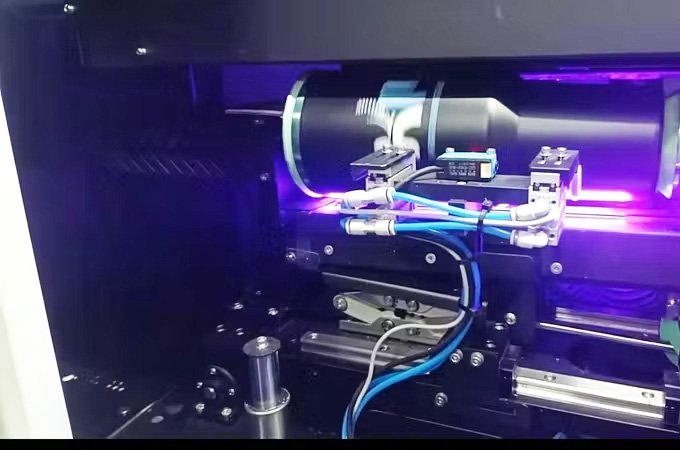
Welding & vacuum insulation
Insulation that holds its promise.
Welded shells move through vacuum insulation technology to improve heat retention.
04
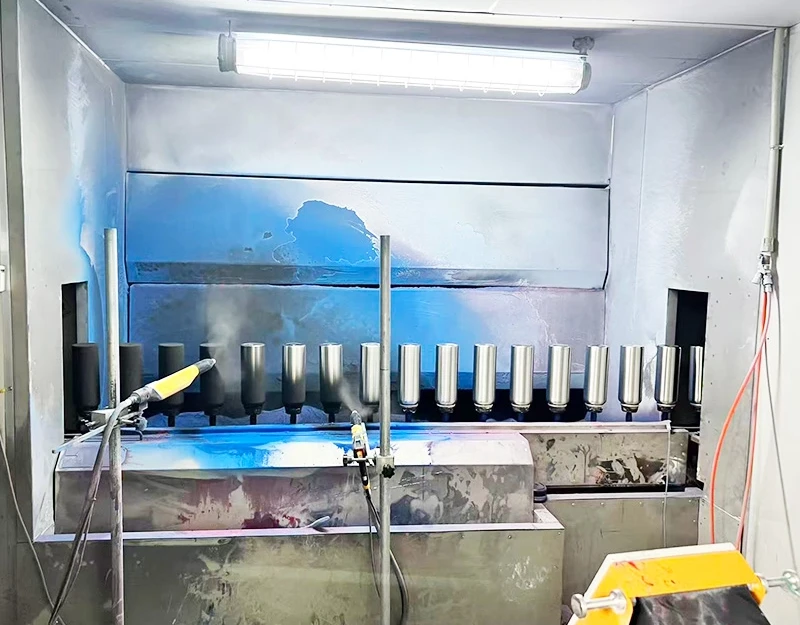
Surface treatment
Finishes made for your brand.
Polishing, powder coating, spraying and printing create smooth, consistent surfaces.
05
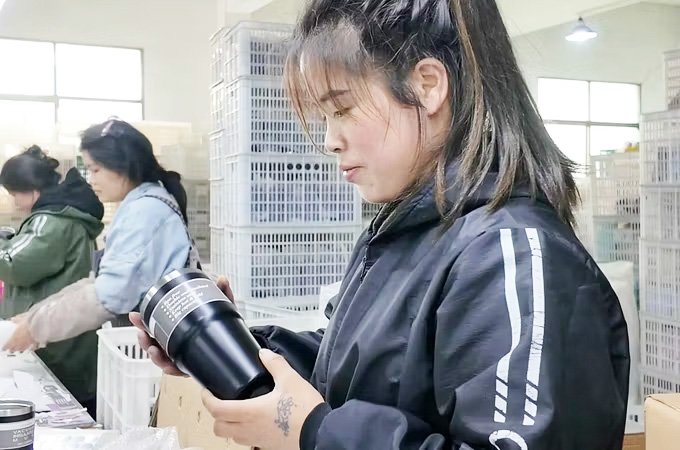
Quality inspection
Nothing leaves unchecked.
Appearance, sealing, vacuum performance and coating quality are reviewed before packing.
06
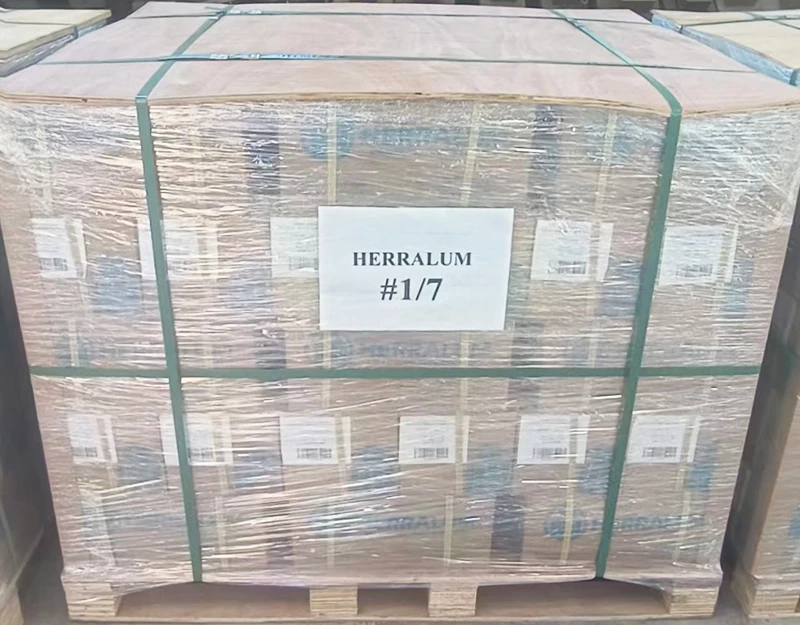
Packaging & shipment
Ready for the next destination.
Products are packed, labeled and prepared for efficient export service worldwide.
Inspection protocol
Our 4-step inspection process.
We do not just manufacture. We verify excellence against the standards your customers expect.
01
IQC: Material verification
Before any coil enters our warehouse, spectrometer analysis verifies the correct Nickel/Chromium ratios for SUS304 (18/8).
Composition check for food-grade stainless steel
Lead-free and BPA-free material screening
02
100% vacuum insulation test
Every double-wall vessel is tested for heat retention, rather than relying on random sampling.
Automated temperature-sensing line
Any heat transfer to the outer wall is rejected
03
Coating & logo durability
Destructive testing protects the brand image on every custom logo tumbler.
Cross-cut test with industry-standard 3M tape protocols
Dishwasher simulation across 20+ wash cycles
04
FQC & pre-shipment
Final quality control follows AQL 2.5 (Major) / 4.0 (Minor) before commercial orders leave the facility.
Drop test from a 1-meter height
Leak-proof shaking test with boiling water
In-house laboratory
Testing with hard data.
We validate manufacturing precision before mass production orders are released.
LAB / 01
Thermal performance test
BS EN 12546-1:2000
Filled with 95°C water, the vessel must remain above 55°C after 24 hours, depending on capacity.
Material composition
Confirming the alloy is consistent with the approved specification.
Coating adhesion
Cross-cut testing ensures the finish stays attached to the surface.
Leakage proof
Sealing and lid interfaces are checked before packaging.
Talk to our team
Start your risk-free inquiry today.
Do not just take our word for it. Request a sample, share your OEM / ODM brief and experience the engineering standard behind our production.